
HBM Memory PCB Manufacturing Challenges: How to Vet HDI and Multilayer Suppliers for Warpage, Micro-Via, and Heavy Copper Risks
Building a board around HBM is harder than the datasheet suggests. Learn
I have been considering switching my PC board fabrication supplier. The previous one kept failing on details — blurry silkscreen, burrs along board edges. The price was slightly lower, but every delivery required half a day of visual inspection. Whatever cost savings the lower price created were consumed by labor.
Choosing a supplier purely on the quoted unit price is a mistake that looks obvious in retrospect. Some manufacturers itemize engineering fees and test fees in ways designed to make total cost look lower than it actually is. When the real invoice arrives, the total bears little resemblance to the initial quote. I place significant weight on whether a supplier has a complete quality traceability system — particularly when the product is a medical device where reliability requirements are non-negotiable.
A common misconception about PC board fabrication: a well-drawn schematic is sufficient to guarantee a good board. The actual quality of the finished product is determined by dimensional control and test procedures — details that exist entirely outside the schematic.
A board I designed years ago had a sensible layout but ignored hole diameter tolerance at plated through-holes. Components could not align correctly during soldering. The near-scrapped batch made the lesson permanent: elegant line art on a drawing means nothing until it survives the manufacturing process.
Before submitting any design files now, I review all critical dimension tolerances — especially in areas where press-fit components will be seated. When a factory pushes back and says a tolerance requirement is too tight, that is actually a good sign. It means they are engaging seriously with the manufacturing precision question. For BGA footprint areas, I specify hole diameter tolerances within ±0.05 mm. Standard through-holes can be relaxed to ±0.1 mm. Differentiated tolerance management effectively balances quality against cost.
For high-frequency signal boards, standard electrical testing is not sufficient. Even after passing conventional continuity and isolation checks, signal integrity may fall short in use. I now routinely request TDR test data and use a vector network analyzer to spot-check impedance continuity on key transmission lines, targeting phase consistency within 5%.
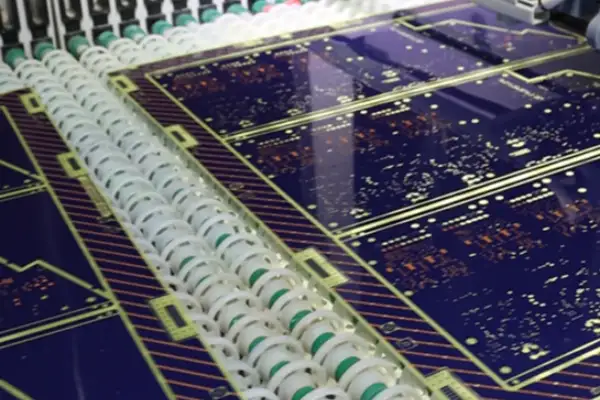
Different base materials behave differently at elevated temperatures, and that variation directly affects dimensional tolerance. An FR4 board I used for a precision instrument experienced micro-scale thermal expansion of solder pad pitch as ambient temperature varied. Switching to a low-loss high-frequency material resolved the issue. For thermally challenging applications, I now specify Rogers 4350B or similar materials as a default — its Z-axis thermal expansion coefficient of approximately 40 ppm per degree Celsius compares favorably to standard FR4 at around 300 ppm per degree Celsius.
The fabrication process should be an ongoing conversation between designer and manufacturer. Designers need to understand process constraints; manufacturers need to provide honest feedback about what creates difficulty in production. I have seen too many straightforward problems become complex because the two sides did not communicate — when a simple routing adjustment could have avoided a tight-tolerance region entirely. On one four-layer board project, the factory suggested converting blind vias to through-holes; yield improved from 70% to 95% as a direct result. That kind of experience only accumulates through sustained collaboration.
A practice I now use consistently: classify critical dimensions by tier. Dimensions that directly affect functional performance receive the highest tolerance specification. Decorative or auxiliary dimensions are relaxed. Power module pad dimensions get ±0.1 mm. Silkscreen label placement can tolerate ±0.3 mm. The factory gains adjustment room during photolithography alignment, and overall board cost stays controlled without compromising function.
A medical device customer once insisted on ENIG for an application where standard HASL would have been entirely adequate. The additional cost was approximately 30%. At the other extreme, a consumer electronics product saved a few dollars per board by specifying an inferior solder mask ink — and arrived at the customer with delaminated solder mask after transit. Neither decision was well-considered.
Surface finish selection should follow application requirements, not assumptions about prestige. ENIG is appropriate where fine-pitch component soldering or repeated probe contact is required. HASL performs reliably for less demanding applications and reduces cost. The cost premium of ENIG makes sense when the application genuinely requires it, and represents waste when it does not.
Solder mask color is another area where engineering substance matters more than visual preference. Green remains the dominant choice for a functional reason: it provides the highest contrast for visual inspection, making it easier to detect defects. White solder mask on LED boards is selected for light reflectance. Black solder mask in high-temperature environments can affect thermal dissipation efficiency. Color selection should follow these engineering considerations rather than aesthetic preference.
Many engineers reflexively pursue the newest technologies. For small-batch development projects, traditional photoplotting may be more economically appropriate than laser direct imaging, even though LDI offers superior resolution. The key is understanding your actual requirement and selecting the process that serves it — not following trends.
Film-based processes are increasingly rare as factories transition to fully digital workflows. Traditional film introduces dimensional variation from temperature and humidity fluctuations during exposure. Digital processes eliminate this by reading Gerber data directly. Current LDI equipment can achieve resolution below 20 micrometers, which is critical for HDI boards with microvia structures and fine-pitch components.
Direct imaging technology offers another practical advantage: it automatically compensates for minor substrate deformation by scanning registration marks and adjusting exposure parameters in real time. For differential pair impedance-controlled designs, line width accuracy can be maintained within ±0.01 mm — a meaningful contribution to high-speed signal integrity.
Etching is a step that reveals process discipline more than almost any other. Chemical bath concentration off by a small amount, or timing not tightly controlled, and circuit edge definition degrades. A friend’s project failed not because of a design error but because the factory was shortcutting the etch time control. Line width uniformity across the batch was inadequate. Hidden process shortcuts of that kind do not surface during sample evaluation. They emerge at volume production.
Post-etch cleaning is equally important and equally easy to cut. Residual chemical contamination that is not fully removed affects solder mask adhesion in the subsequent step. A batch of boards that appeared perfect on visual inspection and passed all standard electrical tests still failed — the cause was contamination that affected adhesion quality during wave soldering downstream. The supplier had simply skipped the cleaning verification step because the specification did not explicitly require it.
Incremental fabrication approaches using additive techniques are being explored in some factories — printing circuits directly to reduce chemical waste. For now, the subtractive etching process remains dominant, and the priority should be executing each step reliably rather than chasing novel methods.
Mechanical drilling handles standard boards adequately but produces burrs more easily on thick boards or high-frequency laminate materials. Laser drilling offers substantially higher positional accuracy, at higher cost — a trade-off appropriate for HDI designs with microvia requirements.
Multi-layer board lamination is where manufacturing complexity peaks. If lamination temperature is even slightly elevated, the prepreg material flows excessively and circuit traces shift in position. Insufficient pressure produces delamination. One eight-layer board project consumed more than thirty material sets during trial production before stable lamination parameters were established.
The plating step — often overlooked — ultimately determines board service life. Factories that reduce plating time to lower cost produce boards whose via walls begin oxidizing and separating within months of deployment. I scrutinize this step specifically. A board that fails at six months represents a much larger cost than any plating premium.
Via structures viewed at board cross-section look like a high-density urban infrastructure — every channel must carry power and signal, must remain stable for the product’s intended service life, and must not fail. That analogy captures why process discipline in drilling and plating matters as much as any upstream design decision.
Running parallel samples at three suppliers simultaneously has become a useful evaluation method. Comparing results across price points consistently reveals that mid-range suppliers deliver the strongest overall performance — board surface cleanliness, solder mask alignment accuracy, and silkscreen registration all tend to exceed both the lowest-cost and the highest-cost options. Spending additional time on upfront supplier selection consistently pays back.
The relationship with a long-term fabrication partner becomes an asset in itself. They understand where your designs tend to be demanding. You understand their process strengths. That mutual calibration is more reliable than any technical specification document. During one production run, the factory proactively flagged that a particular IC pad design was incompatible with their HASL process characteristics. Adjusting before production avoided a quality risk that would not have been visible until the boards were in the field.
When a factory engineer proactively calls to confirm a detail and proposes a better solution, that reflects a quality system with real substance behind it — automated optical inspection on every board, X-ray verification of BGA plating uniformity, impedance coupon analysis for production consistency. Good manufacturers build those capabilities and use them; they do not mention them only in sales presentations.
The principle that guides my fabrication decisions: build from reliable manufacturing fundamentals rather than pursue the most advanced available process. A clean, well-executed double-sided board with a properly designed ground plane may outperform an unnecessarily complex multi-layer design in terms of real-world interference immunity. What matters is that every design decision — current path efficiency, thermal management approach, assembly complexity — reflects an understanding of how the board will actually function, not what it looks like in a cross-section photo.
Building a board around HBM is harder than the datasheet suggests. Learn
Gas leak detector PCBs drift from humidity leakage, residue, and laminate variation,
Submerging a server board in coolant shifts microstrip impedance, swells solder mask,
- Experte für die Produktion kleiner bis mittlerer Chargen
- Hochpräzise PCB-Fertigung und automatisierte Montage
- Zuverlässiger Partner für OEM/ODM-Elektronikprojekte
Geschäftszeiten: (Mo-Sa) von 9:00 bis 18:30
Get quote, solution or any question, Andre always here to help